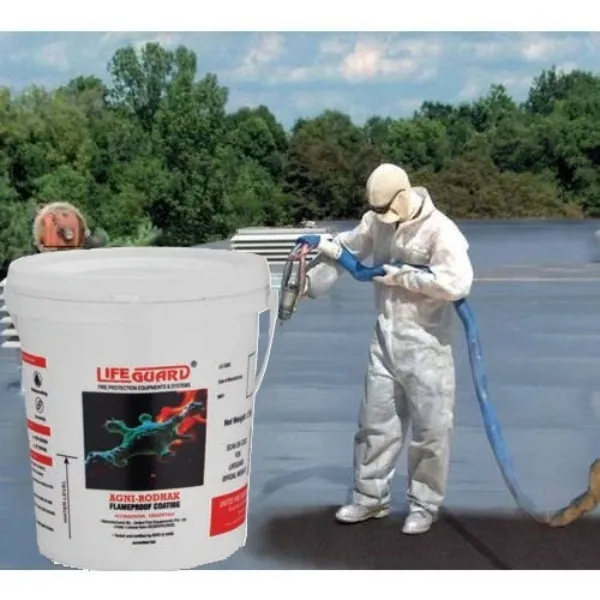
Industrial Waterproof Fire Coating: Dual Protection Against Fire and Moisture
Advanced Industrial Waterproof Fire Coating for Maximum Asset Protection
Industrial facilities operate in challenging environments where structures and equipment are exposed to fire hazards, moisture, humidity, chemicals, and harsh weather conditions. While traditional fire protection solutions focus on fire resistance alone, modern industries increasingly require coatings that provide both fire protection and waterproofing capabilities.
An Industrial Waterproof Fire Coating delivers comprehensive protection by combining fire-resistant performance with superior resistance to water penetration, corrosion, and environmental degradation. At LIFEGUARD®, we provide advanced passive fire protection coatings engineered to safeguard industrial assets, structural steel, and critical infrastructure while extending service life and reducing maintenance costs.
What is an Industrial Waterproof Fire Coating?
An Industrial Waterproof Fire Coating is a specialized protective coating designed to provide dual functionality:
- Fire resistance during fire emergencies
- Waterproof protection against moisture and environmental exposure
These coatings form a durable protective barrier that helps preserve structural integrity, delay heat transfer, and protect surfaces from corrosion and water damage.
They are widely used on:
- Structural steel
- Industrial buildings
- Manufacturing facilities
- Warehouses
- Power plants
- Oil & gas installations
- Offshore structures
- Electrical rooms
- Cable trays
- Infrastructure projects
Why Industries Need Waterproof Fire Coatings
Industrial assets often face multiple threats simultaneously. Fire incidents can cause catastrophic losses, while moisture exposure can lead to corrosion, deterioration, and reduced structural performance.
Waterproof fire coatings help address both challenges by providing:
Fire Protection
Enhances fire resistance and delays structural failure during fire exposure.
Moisture Resistance
Prevents water ingress and protects substrates from environmental damage.
Corrosion Control
Reduces the risk of rust formation on steel structures.
Extended Service Life
Improves durability and reduces maintenance requirements.
Cost Savings
Minimizes repair, replacement, and lifecycle costs.
Key Features of Industrial Waterproof Fire Coatings
Superior Fire Resistance
Creates a protective thermal barrier that reduces heat transfer during fire incidents.
Waterproof Performance
Provides long-term protection against rain, humidity, condensation, and water exposure.
Corrosion Resistance
Protects steel and metal surfaces from oxidation and corrosion.
High Durability
Designed to perform in demanding industrial environments.
Weather Resistance
Maintains performance under varying climatic conditions.
Excellent Adhesion
Ensures long-lasting protection on a wide range of industrial substrates.
Low Maintenance
Reduces the need for frequent repairs and recoating.
How Industrial Waterproof Fire Coatings Work
These advanced coatings form a protective layer over the substrate. Under normal conditions, they act as a waterproof barrier that prevents moisture penetration and environmental damage.
During a fire event:
- Heat transfer is slowed
- Structural temperatures rise more gradually
- Fire spread is reduced
- Structural stability is maintained for longer periods
- Damage to critical assets is minimized
Many systems incorporate advanced passive fire protection technologies that enhance insulation and fire resistance under extreme temperatures.
Applications of Industrial Waterproof Fire Coatings
Manufacturing Plants
Protect production facilities, structural steel, machinery supports, and utility infrastructure.
Warehouses and Logistics Centers
Safeguard storage structures and inventory protection systems.
Power Plants
Protect turbines, transformers, cable trays, and structural frameworks.
Oil & Gas Facilities
Provide protection in high-risk environments exposed to fire hazards and harsh weather conditions.
Chemical Processing Plants
Enhance safety and durability in corrosive industrial settings.
Electrical Rooms
Protect electrical infrastructure against both fire and moisture-related risks.
Offshore Platforms
Provide critical protection against saltwater exposure and fire hazards.
Infrastructure Projects
Protect bridges, tunnels, airports, metro stations, and transportation facilities.
Benefits of Waterproof Fire Coatings for Industrial Facilities
Enhanced Structural Protection
Protects load-bearing structures from fire and environmental damage.
Improved Asset Reliability
Extends the lifespan of industrial infrastructure and equipment.
Reduced Downtime
Minimizes maintenance interruptions and fire-related operational losses.
Business Continuity
Supports uninterrupted operations through improved facility resilience.
Regulatory Compliance
Helps meet industrial fire safety and infrastructure protection standards.
Long-Term Cost Efficiency
Reduces maintenance, repair, and replacement expenses over the life of the asset.
Industrial Waterproof Fire Coatings and Passive Fire Protection
Passive Fire Protection (PFP) remains one of the most effective methods of safeguarding industrial facilities. Unlike active systems such as sprinklers and alarms, passive fire protection works continuously without activation.
Waterproof fire coatings contribute to passive fire protection by:
- Protecting structural steel
- Reducing heat transfer
- Enhancing fire resistance ratings
- Limiting fire spread
- Preserving structural integrity
- Supporting safe evacuation
This dual-protection approach delivers exceptional value for industrial environments.
Why Choose LIFEGUARD® Industrial Waterproof Fire Coatings?
Advanced Protection Technology
LIFEGUARD® coatings are engineered to provide both fire resistance and environmental durability.
Industrial-Grade Performance
Designed for demanding manufacturing, infrastructure, and energy-sector applications.
Long-Term Durability
Offers dependable protection against fire, water, humidity, and corrosion.
Expert Technical Support
Our specialists assist with product selection, project specifications, and application guidance.
Quality-Assured Solutions
Every product undergoes rigorous testing to ensure consistent performance and reliability.
Future-Proof Your Industrial Assets with LIFEGUARD®
Modern industrial facilities require protection that goes beyond conventional fireproofing. Industrial Waterproof Fire Coatings provide a comprehensive solution that enhances fire safety while protecting structures from moisture, corrosion, and environmental degradation.
LIFEGUARD® delivers innovative coating technologies that help industries improve safety, increase durability, reduce maintenance costs, and protect valuable assets for years to come.
Contact LIFEGUARD®
LIFEGUARD® – United Fire Equipments Pvt. Ltd.
Manufacturer of ISI Certified Fire Safety Equipment
📞 8048034226
Keywords